Fastener Supplier Factory Audit: An 8-Step Checklist for Verifying ISO/DIN Standard Compliance Capability

Daniel
With experience in fastener manufacturing and export sales, we specialize in bolts, nuts, screws, self-drilling screws, fully threaded rods, and customized fastening solutions for construction, machinery, automotive, and industrial applications.
Introduction: Complete certificates do not mean every batch of products meets standards
In fastener procurement, the most common misjudgment is that "complete certificates equal reliable quality." In reality, there is often a clear gap between the ISO 9001 certificates, inspection reports, or the "DIN standard" wording in brochures provided by suppliers and whether each batch of screws and nuts truly meets standards. Risks that procurement personnel frequently encounter include: the scope covered by certificates not matching actual production, incorrect drawing versions used in production, missing batch traceability records, and batch-to-batch fluctuations in the dimensions or mechanical properties of screws and nuts.
In ordinary assembly, these problems may only lead to rework, but in equipment subjected to cyclic loads, temperature changes, or pressure conditions, they may cause connection failure, leakage, or even safety accidents, along with delivery delays and customer claims. Therefore, the core of a factory audit is not "looking at certificates," but verifying whether the supplier has the capability to continuously and stably produce products that meet standards.
This article provides an on-site executable 8-step factory audit checklist to help procurement personnel verify fastener suppliers' standard compliance capabilities item by item. It should be specially noted that ISO and DIN belong to different standard systems, and the dimensions, tolerances, property grades, and marking requirements for the same type of product under different systems do not fully correspond. Verification should be based on procurement contracts, controlled drawings, product standards, and applicable versions, and vague statements such as "compliant with ISO/DIN" should not be accepted indiscriminately.
Step 1: Verify standards, drawings, and order requirements
The first stop of a factory audit should be documents, not the workshop. Require the supplier to confirm item by item the product name, specifications, material, property grade, surface treatment, tolerances, and inspection requirements, and to record in writing the applicable ISO, DIN, or customer standards and their version numbers. For example, for the same hexagon socket head cap screw, ISO 4762 and the older DIN 912 differ in some details and cannot be assumed to be interchangeable.
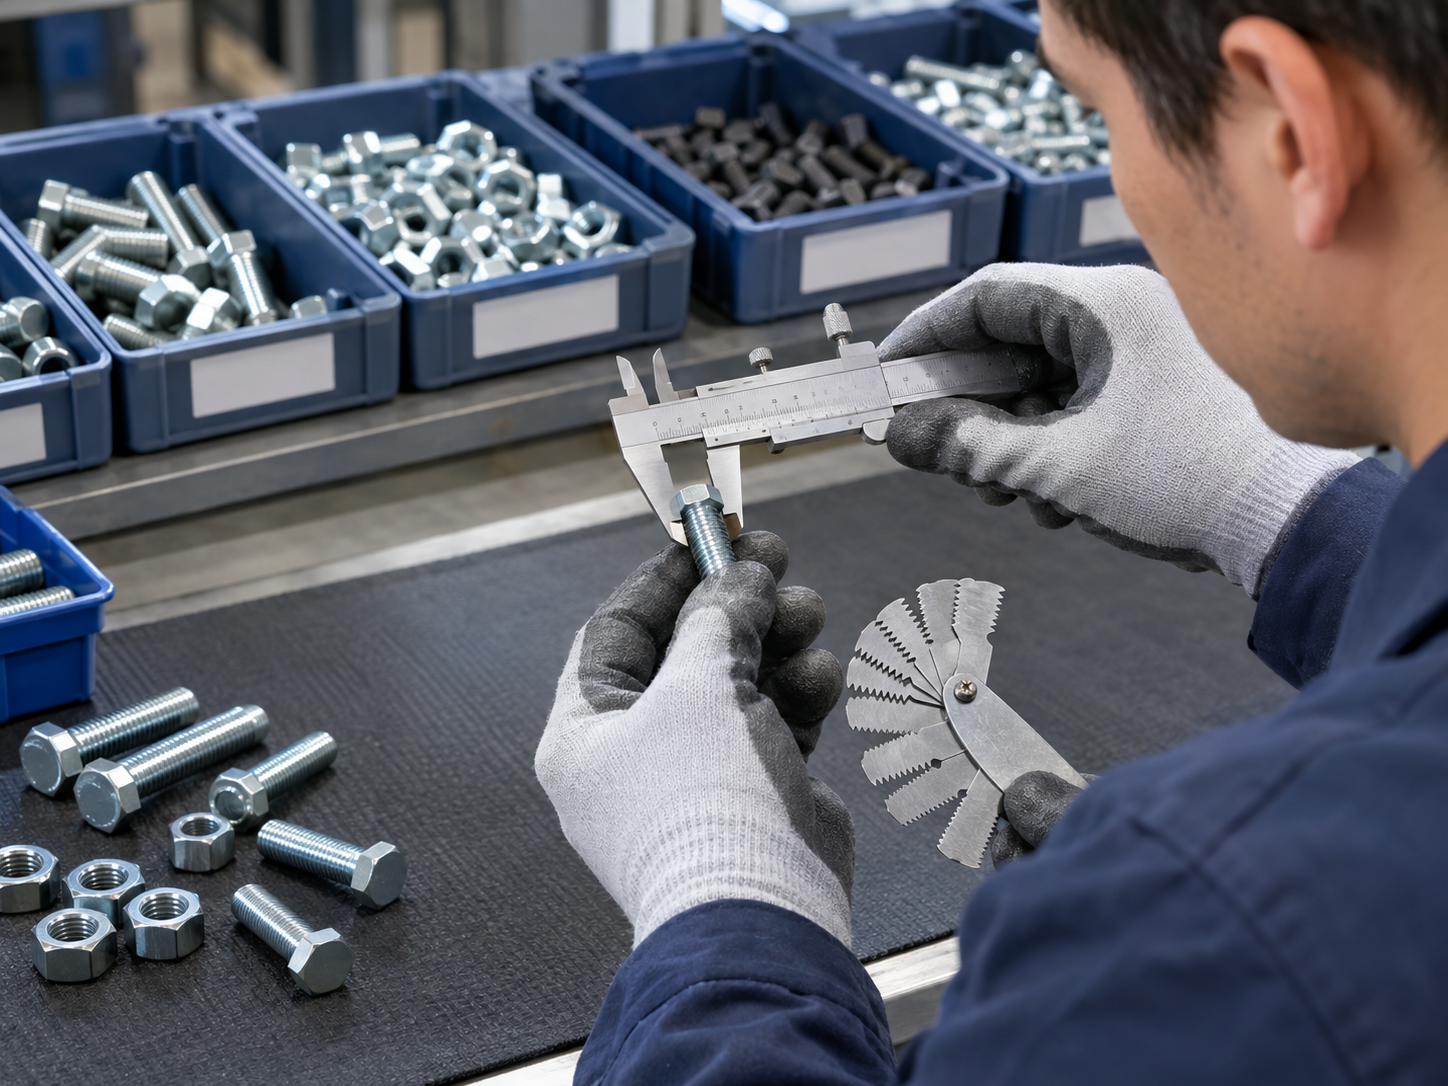
At the same time, check whether the supplier can clearly distinguish products with similar standards that cannot be arbitrarily substituted, such as hex bolts, flange bolts, and different types of nuts. Take cross-recessed countersunk head machine screws as an example: DIN 965 specifies the countersunk angle, recess type, and thread specifications, and they are commonly used in electrical equipment, furniture, and panel assembly; if the supplier mixes similar specifications or substitutes them based on experience, problems such as the countersunk head not fitting flush and the recess type not matching the driver bit will occur during assembly. For custom hex socket screw projects, it should also be confirmed whether the supplier can accurately convert customer drawings rather than applying existing molds.
Require the supplier to provide controlled drawings, a standards list, and order technical review records; for custom products, the drawing version number and change approval process should be confirmed. On site, a direct question can be asked: are the standards and versions cited in the quotation, samples, production work orders, and inspection documents completely consistent? Any inconsistency is a hidden risk of subsequent batch deviations.
Step 2: Confirm that certificates are authentic and cover actual business
When checking quality management system certificates, verify the validity period, certification body, and certification scope, and verify authenticity through the certification body's official channels. Many procurement disputes stem from inconsistency between the certificate address, legal entity, and actual production site—mistaking a certificate held by a trading company for proof of a factory's production capability is a common trap in fastener procurement.
More importantly, confirm whether the system documents are truly implemented in the incoming material, process, inspection, and shipping stages of specific products such as bolts and nuts. A recent order can be randomly selected, and the supplier can be asked to show the corresponding records for that order in the system documents. For fastener export suppliers that handle both domestic sales and inch-series bolt exports, it should also be confirmed whether their document system can meet the documentation and declaration of conformity requirements of export orders.
It must be noted that system certification cannot replace product testing, material certificates, or batch conformity documents. ISO 9001 certifies the quality management process, not the dimensional and performance conformity of a particular batch of screws.
Step 3: Trace raw materials and supplier sources
Raw material traceability is a key link in judging the management level of a fastener manufacturer. Spot-check raw material procurement records, material certificates, heat numbers or batch numbers, and verify their correspondence with production work orders and finished product labels. Material grades, chemical composition, and mechanical property requirements must match the order; for stainless steel fasteners, particular attention should also be paid to material grades (such as the 304 and 316 series) and mixed-material prevention management, because different grades look similar, and the difference in corrosion resistance after mixing is significant.
Check whether products such as carbon steel nuts and alloy steel bolts have clear approved supplier management and incoming material acceptance standards. For high-strength bolt manufacturers, the stability of material sources directly determines whether property grades can stably reach 8.8, 10.9, or higher; for hot-dip galvanized bolt suppliers, incoming material and process control records related to the zinc coating should also be confirmed.
A verification question can be asked on site: can a finished product be traced back to the raw material batch, supplier, and inspection records? If traceability breaks at any stage, it indicates that the supplier's batch management is not yet sufficient to support a declaration of standard conformity.
Step 4: On-site verification of equipment, processes, and process control
Inspect forming, machining, thread rolling, heat treatment, and surface treatment process by process along the production flow to confirm that the actual process matches the order requirements. Review key equipment inspection records, mold management, process parameter records, and abnormality handling records to assess whether production is stable rather than relying on verbal promises. The heat treatment process is particularly critical—the property grades of high-strength bolts and studs depend almost entirely on the control level of quenching and tempering, and batch isolation measures and traceability of parameter records should be verified.
For fastener OEM contract manufacturing, non-standard fastener processing, and custom special-shaped fastener projects, focus on confirming the drawing conversion, first article approval, and change control processes. Take ISO 7380-1 hexagon socket button head screws as an example: their low button head and hex socket drive impose relatively high requirements on head forming and socket depth control, and they are commonly used in mechanical equipment, furniture, and equipment panel assembly; if mold wear management for such products is inadequate, out-of-tolerance head height or driver bit slippage is likely to occur. Similarly, for self-tapping screw manufacturers and self-drilling screw suppliers, the completeness of parameter records for thread forming and heat treatment processes should also be verified on site.
Step 5: Evaluate measuring equipment and inspection capability
Verify the calibration status, range, and suitability of gauges and testing equipment, and spot-check calibration certificates and daily inspection records. Conduct on-site spot measurements of key dimensions, threads, head shapes, and assembly-related characteristics; suitable gauges and inspection methods should be used for screws and nuts, such as go/no-go thread gauges, countersunk angle gauges, and head diameter and height measuring tools.
Confirm that the supplier can carry out inspections related to mechanical properties, hardness, materials, or surface treatment according to order requirements; for special items, the name of the external laboratory and the report management method should be specified. Request to see inspection plans, sampling rules, nonconforming product handling records, and corrective and preventive actions. For machine screw wholesale orders with multiple specifications, it should also be confirmed whether inspection resources can cover all specifications rather than performing full inspection only on main products.
Step 6: Verify batch identification, packaging, and documents
Spot-check the status identification of finished products, semi-finished products, and products awaiting inspection to confirm that different specifications, materials, strength grades, and surface treatments are not mixed in the same batch. Verify whether the product name, specifications, quantity, batch number, and order number on packaging labels are consistent with the actual items and shipping documents. The fastener industry has densely packed specifications; if M6 and M8, grade 8.8 and 10.9, and galvanized and stainless steel are not clearly identified, the risk of mixed batches is extremely high.
Confirm that each order batch can provide inspection reports, material certificates, declarations of conformity, and other necessary documents as agreed. For export orders, verify label, packaging, and documentation requirements; inch-series bolt export projects should be confirmed item by item according to the standards and documents agreed in the contract, and "the same model for domestic sales" cannot be used as a substitute. For products shipped mainly in full cartons, such as expansion bolt wholesale and carriage bolt factories, the accuracy of outer carton markings and packed quantities should also be included in the verification.
Step 7: Audit nonconforming product, complaint, and change management
Review recent nonconforming product, customer complaint, and return records to determine whether problems have root cause analysis, corrective actions, and effectiveness verification. Check the isolation of nonconforming products, rework/repair approval, and scrapping processes to avoid unauthorized substitution or release—for example, substituting lower-strength-grade material for the higher-strength material required by the order is one of the most serious risks in fastener procurement.
Confirm whether changes to materials, processes, equipment, subcontractors, or drawings have been approved by the customer and are traceable through records. For products involving special functions, such as lock nut suppliers and heavy hex nut manufacturers, process changes (such as changes to nylon ring material or spot welding parameters) must be communicated to the customer in advance.
Verification questions can be raised on site: when dimensional deviations or performance nonconformities occur, can the supplier quickly identify the affected batches and propose a verifiable handling plan?
Step 8: Assess delivery, production capacity, and ability to sustain cooperation
Verify order review, production scheduling, delivery monitoring, and capacity planning, and confirm that quotation commitments match actual equipment, personnel, and subcontracting capabilities. Assess peak-season material preparation, inventory management, urgent order handling, and logistics arrangements, with particular attention to the documentation and delivery coordination capabilities of export suppliers.
Set specific questions according to the procurement category: for example, the specialized processes and inspection capabilities for lock nuts, hot-dip galvanized bolts, expansion bolts, or custom bolts; head forming and flatness control for flange bolt suppliers; and mold and lead time management for custom hex socket screw projects. Use trial orders to verify quality, document completeness, and delivery performance; do not replace on-site audits and sample verification with trade shows, social media content, or customer case studies alone.
How to judge factory audit results: establish a scoring and corrective action closed-loop
It is recommended to set scoring items for standards and documents, material traceability, process control, inspection capability, batch management, nonconformity handling, and delivery capability to form a comparable factory audit scorecard. List certificate authenticity, broken batch traceability links, and missing key inspections as high-risk items, and clearly define the conditions for suspending introduction or requiring corrective action within a deadline.
For general gaps, assign responsible persons, correction deadlines, required evidence, and review methods; decide whether to enter the approved supplier list only after corrective actions are closed. Establish annual re-audits, major change re-audits, and quality abnormality-triggered re-audits so that factory audits are not a one-time action but a continuous management tool.
Conclusion: Implement standard requirements in every batch of products
True capability to comply with ISO/DIN requirements should be reflected in controlled documents, on-site processes, inspection data, batch traceability, and continuous improvement, not in a few lines on a brochure. It is recommended that procurement personnel carry this checklist for on-site sample verification and write the standard version, acceptance indicators, and accompanying document requirements into the procurement contract, so that every acceptance has a basis.
The same evidence verification logic applies to various procurement needs: whether looking for fastener manufacturers, hex bolt manufacturers, flange bolt suppliers, stainless steel fastener manufacturers, self-tapping screw manufacturers, or self-drilling screw suppliers, all should undergo the same document, on-site, and data verification. The ultimate purpose of a factory audit is to implement standard requirements in every batch of screws, nuts, and bolts, rather than stopping at the certificate level.

